JoeisaRobot
As the international hospitality, food service, and retail sectors experience rapid post-pandemic revitalization, the demand for high-efficiency, resource-saving dishwashing equipment and automated kitchen solutions has reached unprecedented heights. Modern commercial enterprises no longer view dishware sanitation as a mere back-of-house utility task; instead, it is recognized as a vital pillar of operational hygiene, energy conservation, and strict regulatory compliance.
As a leading manufacturing hub, China has established an unassailable global position in producing industrial washing systems, intelligent vending kiosks, and automated kitchen automation hardware. By integrating advanced IoT telemetry, precision hydraulic design, and eco-friendly thermal recovery systems, Chinese manufacturers deliver unrivaled value propositions to global importers, brand owners, and hospitality chains.
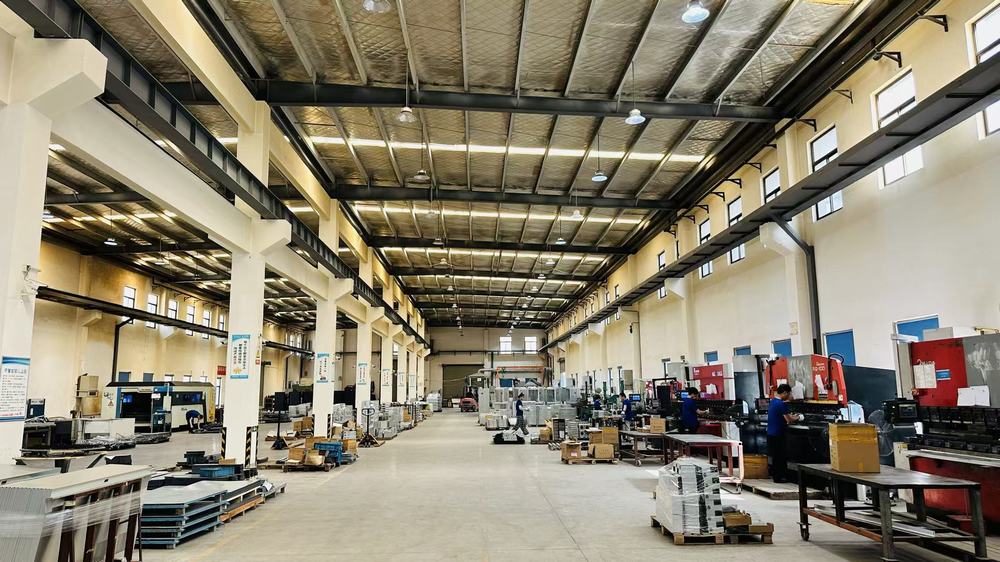
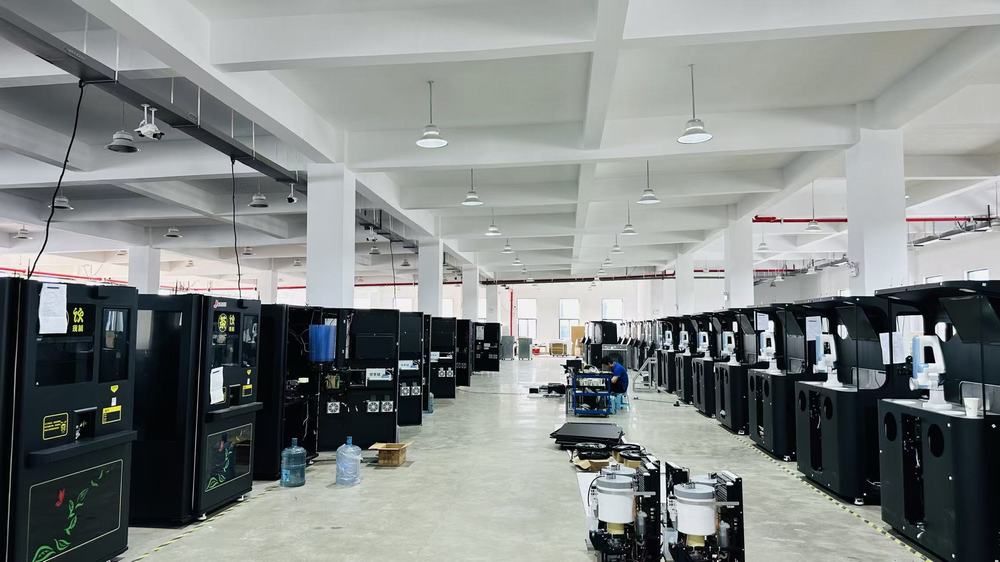
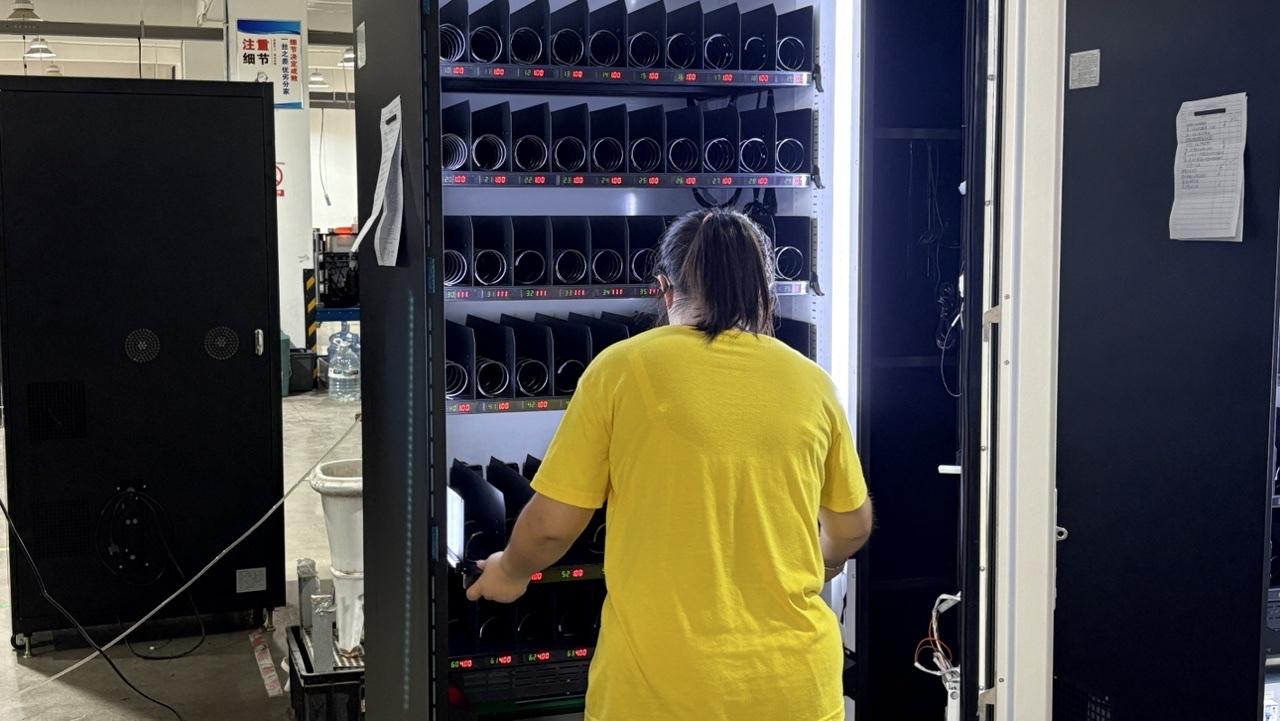
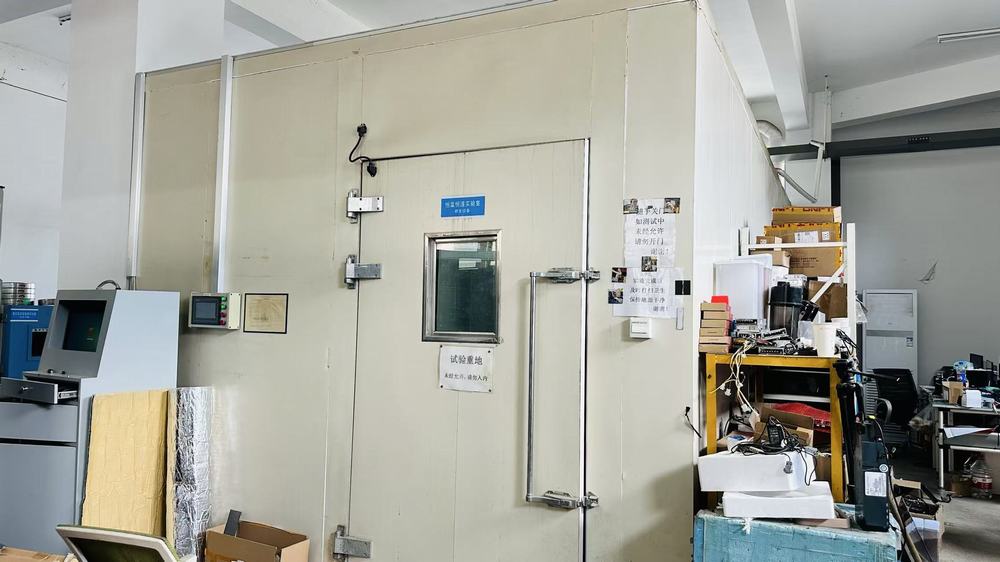
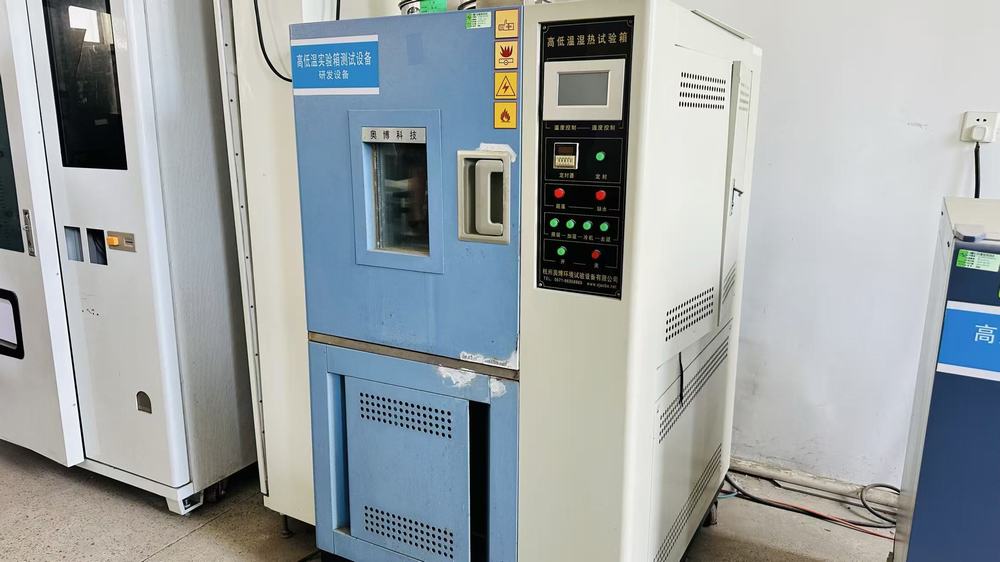
Sourcing from top-tier Chinese manufacturing ecosystems offers global B2B buyers distinct structural advantages. Our 32,496-square-meter state-of-the-art manufacturing plant features 6 fully optimized production lines supported by dedicated R&D teams comprising 15 senior graduate engineers. This robust infrastructure enables us to achieve seamless vertical integration—from raw material traceability and precision sheet metal fabrication to modular electronic assembly and rigorous stress testing.
Furthermore, our streamlined supply chain partnerships ensure optimal cost efficiencies without compromising on premium component sourcing. Whether executing light customization, on-demand prototyping, sample processing, or graphic processing, our agile manufacturing framework adapts dynamically to diverse international market demands across Southeast Asia, North America, Europe, and beyond.
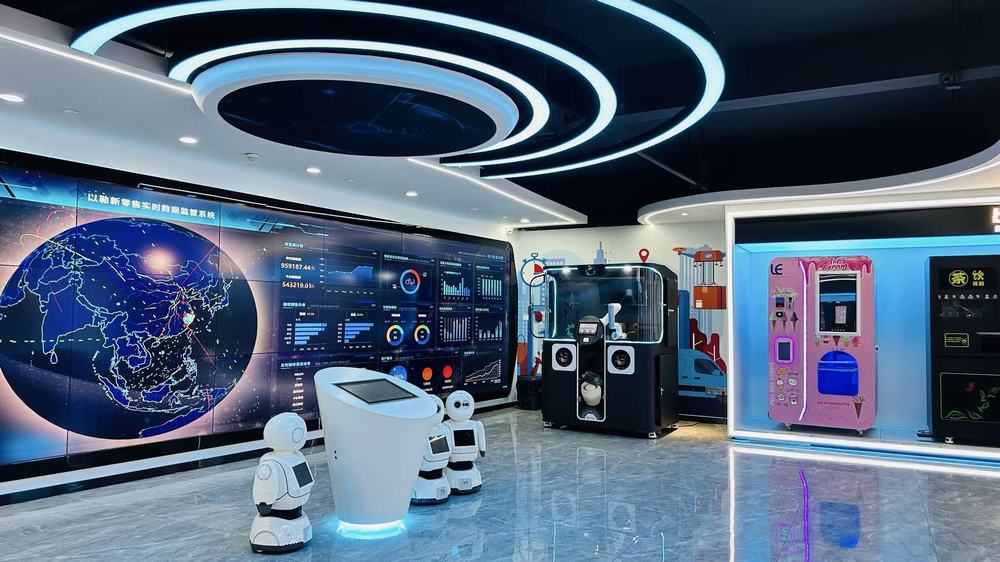
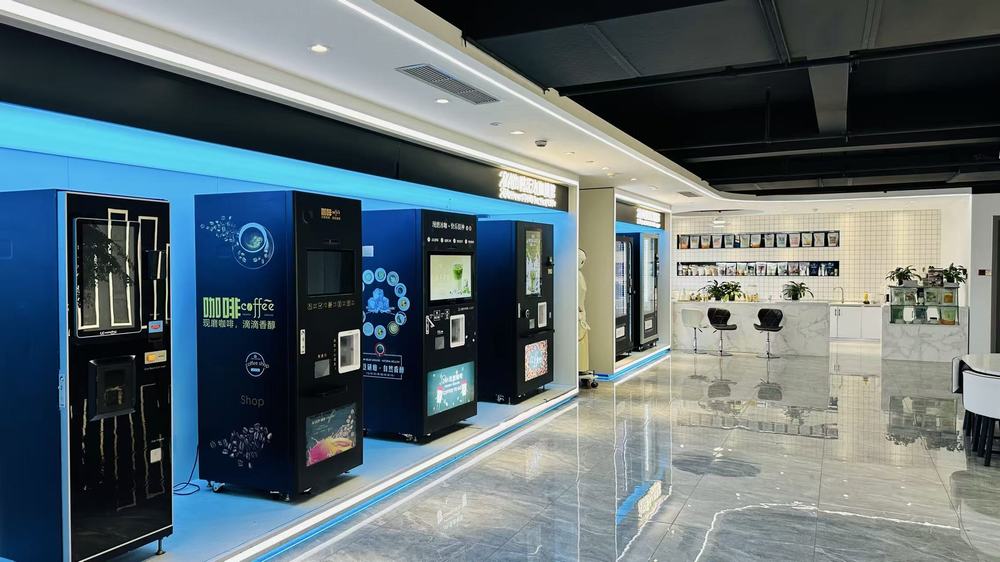
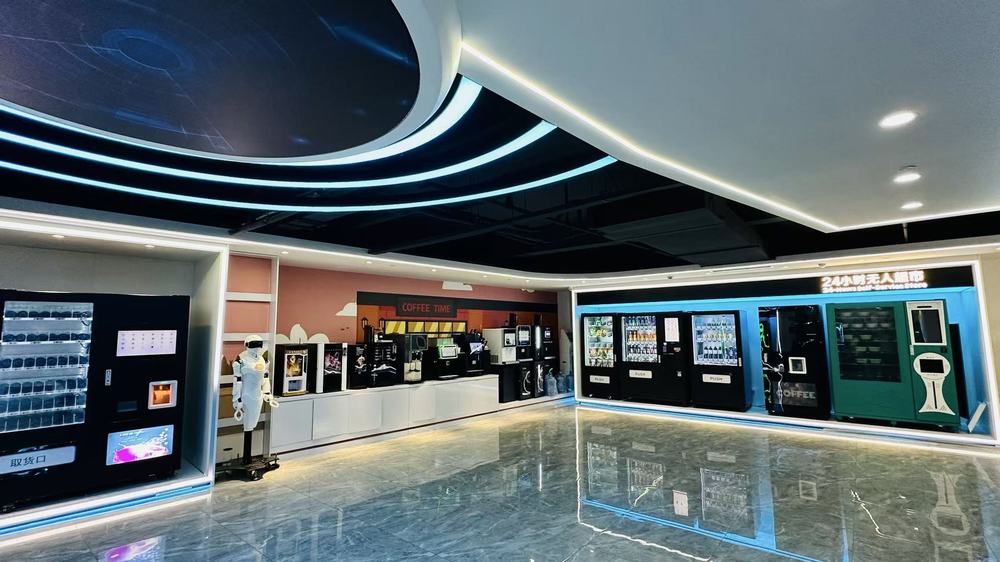
Transparency and operational excellence form the cornerstone of trust in international B2B commerce. Below is a visual showcase of our advanced production lines, precision testing laboratories, and factory floor operations.
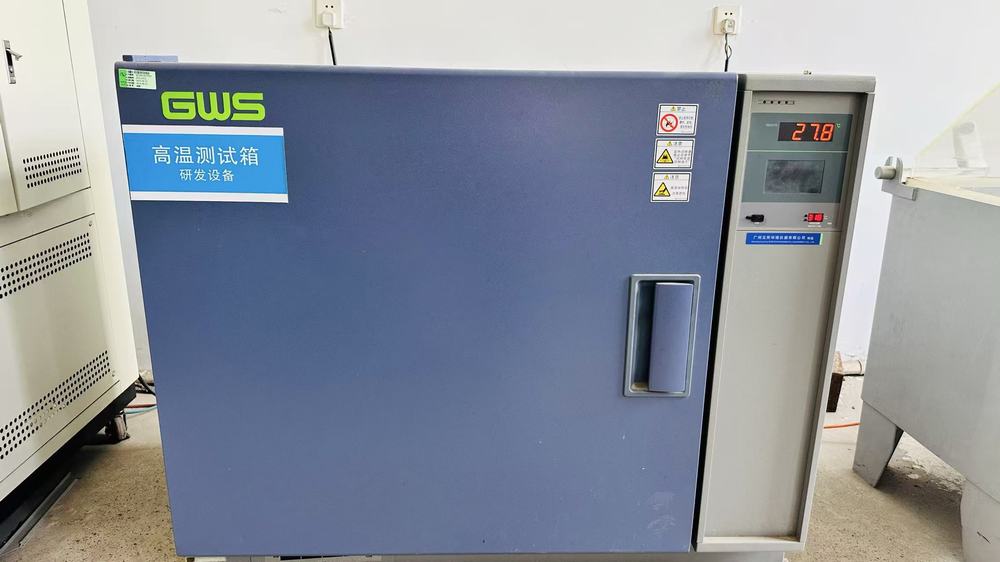
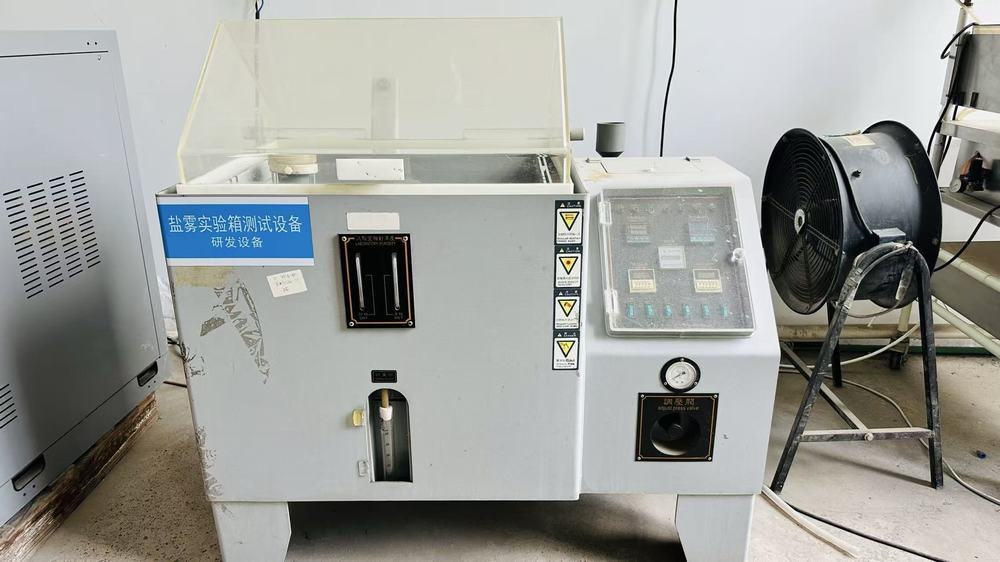
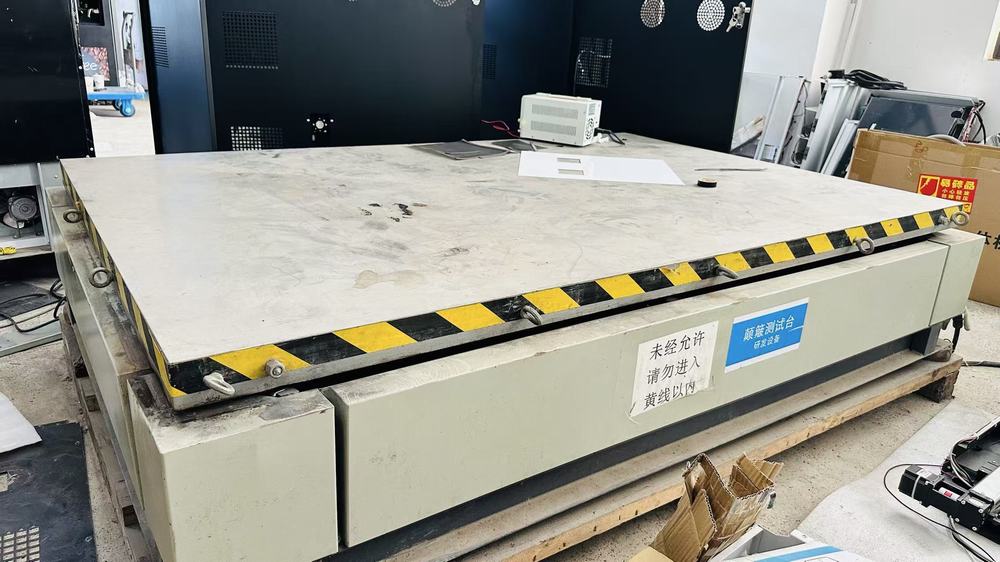
Adhering strictly to international compliance benchmarks, our enterprise holds prestigious certifications verifying our commitment to environmental management, operational quality, and product safety.
Company Registration Date: 2007-11-07
Facility Floor Space: 32,496 ㎡
Industry Experience: 19 Years (Exporting for 19 Years)
Supported Languages: English, Spanish, Italian, Russian
Core Client Segments: Brand Businesses, Retailers, Wholesalers
Primary Export Markets: Southeast Asia (35%), Domestic Market (20%), North America (10%)
ISO 9001 Quality Management: Certified (NOA1827667)
ISO 14001 Environmental Standard: Certified (NOA1998653)
IEC 60335 Electrical Safety: Certified (SHES200701263401-M3)
Raw Material Traceability: Fully Implemented (Yes)
Inspection Protocol: 100% Comprehensive Inspection on All Production Lines by 14 Dedicated QA/QC Inspectors
Commercial dishwashing equipment and automated food service hardware must adapt seamlessly to varying regional infrastructure parameters. Whether deployed in high-footfall transportation hubs in North America, bustling quick-service restaurants in Southeast Asia, or premium hospitality venues in Europe, our machinery incorporates adaptive voltage configurations, localized user interfaces (supporting English, Spanish, Italian, and Russian), and flexible plumbing/drainage adaptations (including air-cooled, water-hookup-free options).
Exporting to highly regulated markets requires uncompromising adherence to international electrical and safety directives. Our equipment undergoes rigorous testing to satisfy IEC 60335, CE, and RoHS standards. By embedding fail-safe thermal sanitization cycles, food-grade stainless steel (SUS304) construction, and advanced IoT diagnostic modules, we guarantee that our global partners meet local health department inspections with absolute confidence.
The next decade of commercial kitchen equipment manufacturing will be defined by smart automation and eco-efficiency. Key trends include real-time predictive maintenance via cloud telemetry, AI-driven water and energy conservation algorithms, and closed-loop heat recovery systems that dramatically lower operational overhead for restaurant operators. As an innovation-driven manufacturer, our R&D roadmap consistently integrates these cutting-edge technologies into our product portfolio.