JoeisaRobot

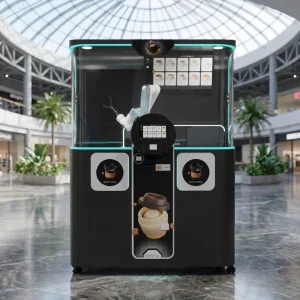
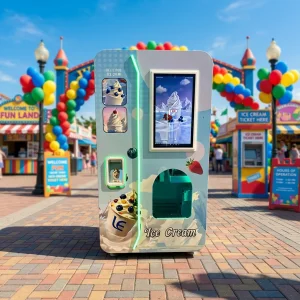
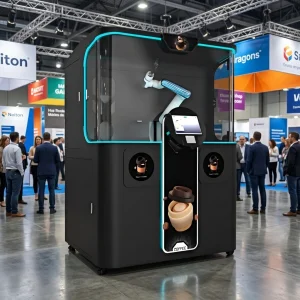
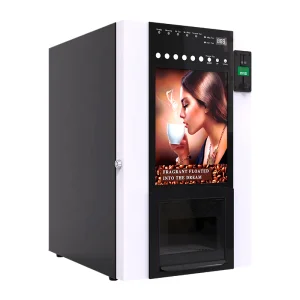
As global culinary demands evolve toward high-efficiency automated cooking systems, partnering with reliable China wholesale deep fryer manufacturers and exporters has become a critical strategic advantage for commercial kitchen distributors, fast-food chains, and hospitality conglomerates worldwide. Leveraging advanced manufacturing clusters, robust supply chain ecosystems, and stringent quality assurance frameworks, Chinese industrial manufacturing provides unparalleled scalability, cost-efficiency, and technological innovation in heavy-duty frying and automated vending machinery.
In alignment with Google’s E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness) guidelines, this whitepaper evaluates the structural advantages of sourcing commercial food-service equipment from certified Chinese manufacturers. It provides deep insights into compliance standards, localized customization capabilities, technological integration (such as IoT and smart SDK management), and global logistical support.
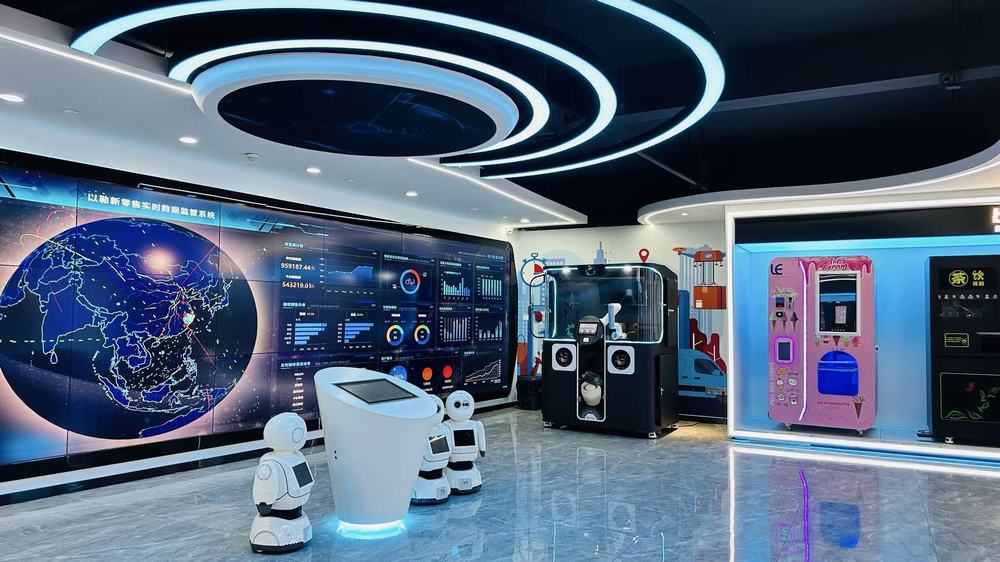
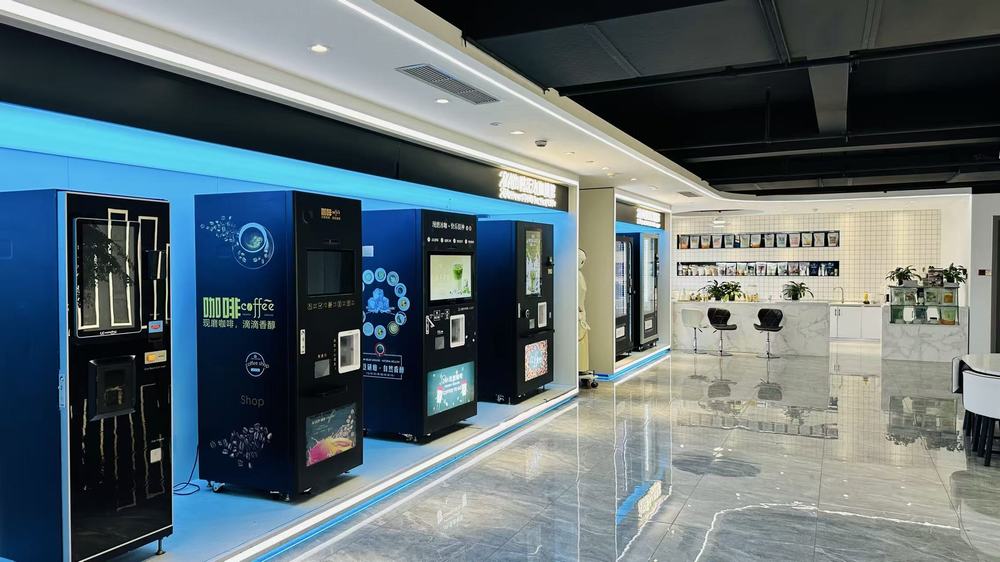
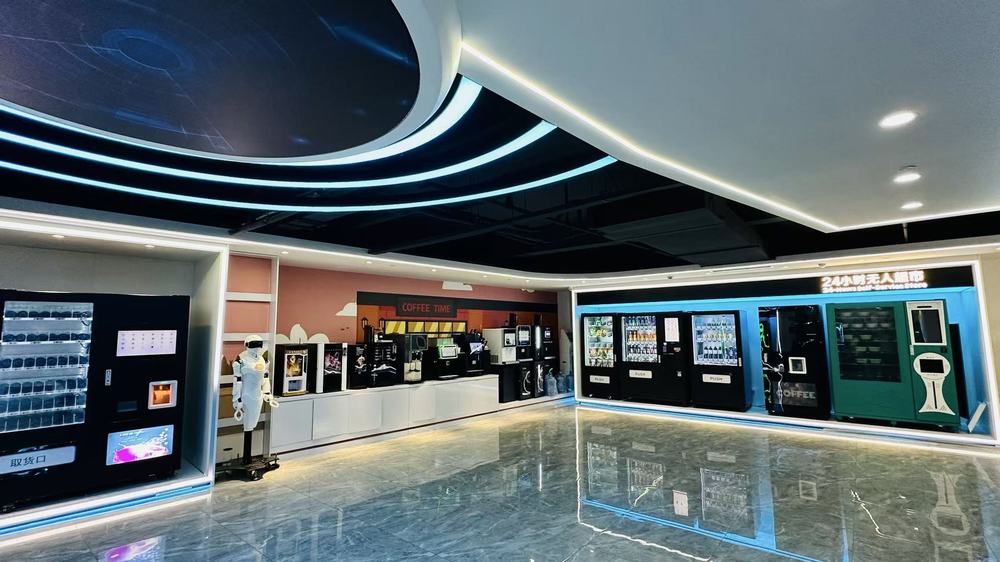
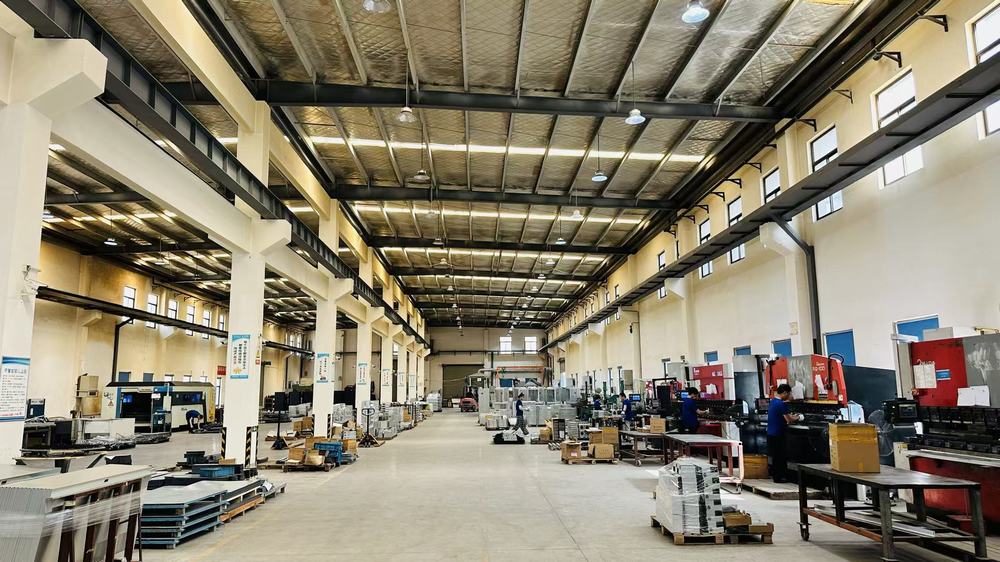
Chinese manufacturing hubs possess integrated ecosystems covering raw material procurement (food-grade stainless steel 304/316), precision laser cutting, automated robotic welding, and advanced electrical assembly. This complete localization of supply chain components drastically reduces lead times and production costs while maintaining strict tolerance levels required for commercial-grade kitchen appliances.
Modern commercial deep fryers and automated food machinery are no longer standalone mechanical units. Industry leaders are integrating cloud-based management systems, SDK functions, touch-screen interfaces, and automated oil filtration technologies. These innovations empower global operators with remote diagnostics, inventory monitoring, and precise temperature control.
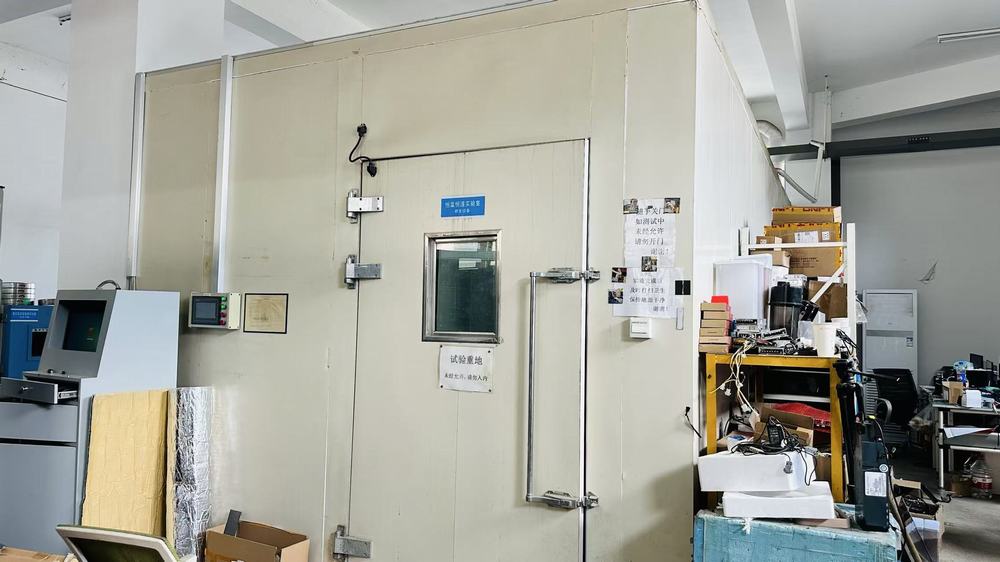
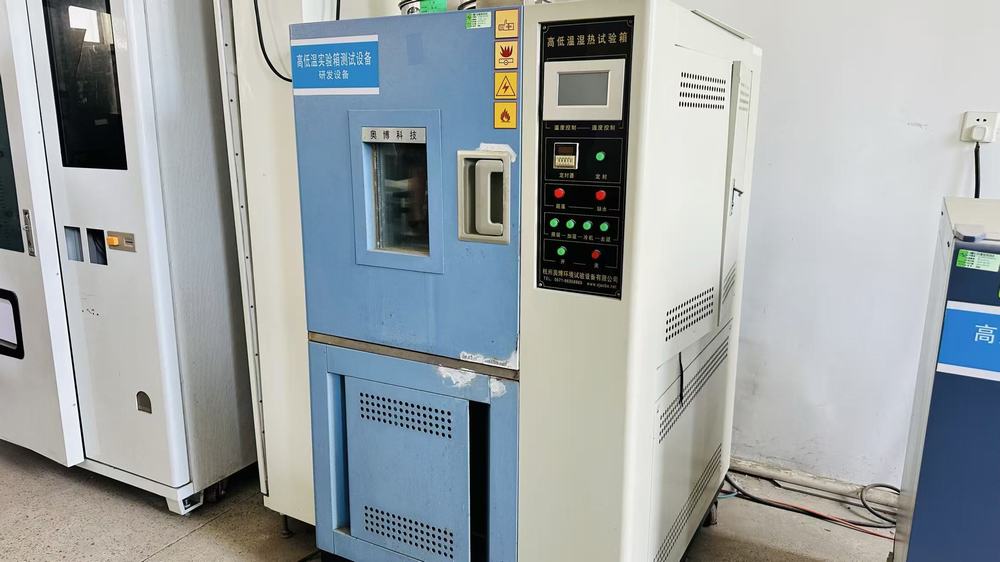
 ISO 9001 Quality Management
Certificate No: NOA1827667
 ISO 14001 Environmental Management
Certificate No: NOA1998653
 IEC 60335 Electrical Safety
Certificate No: SHES200701263401-M3
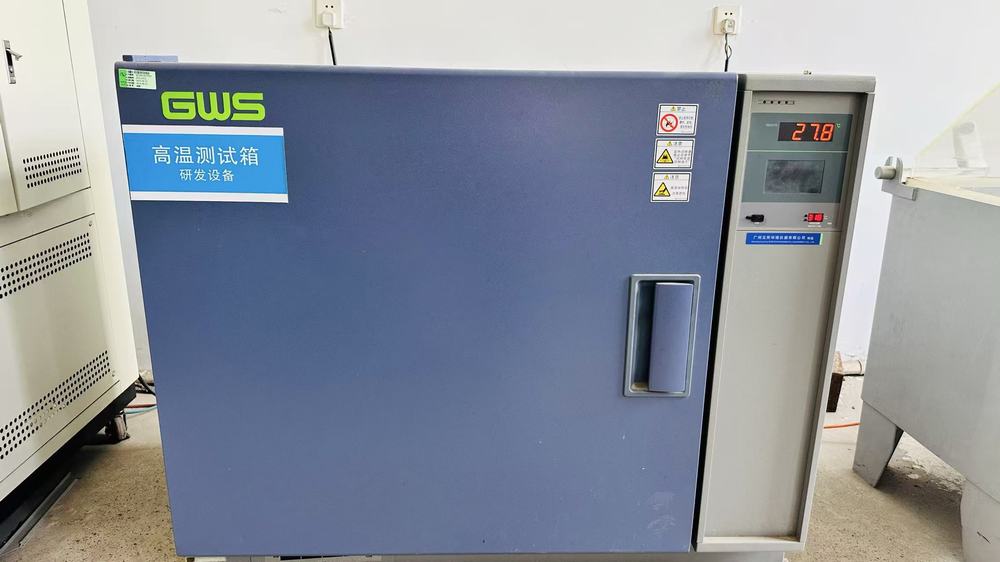
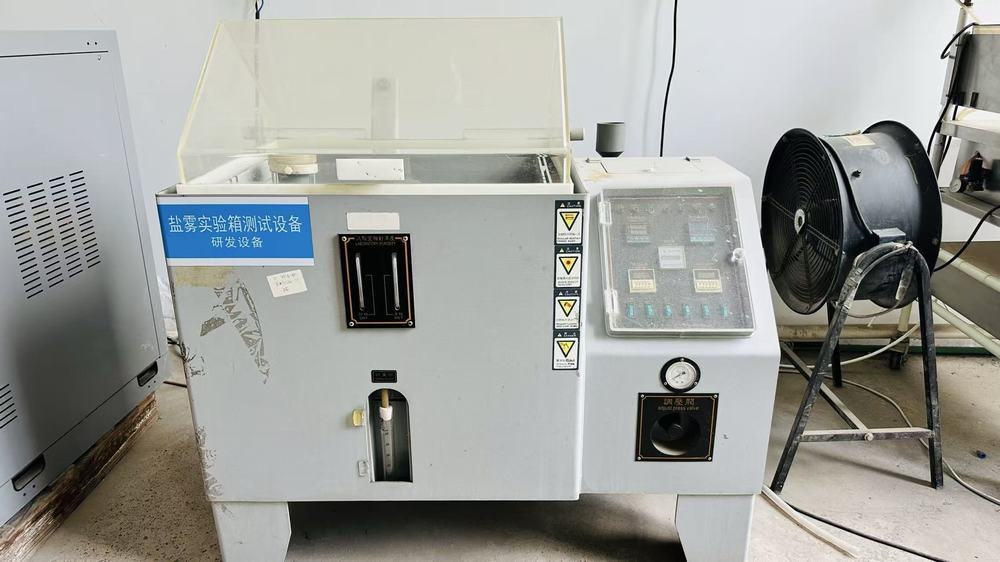
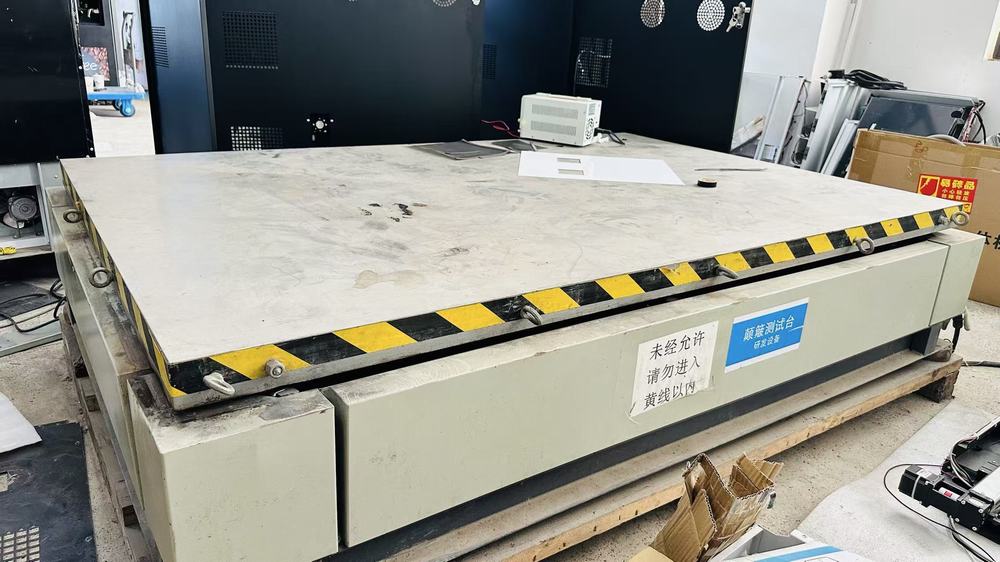
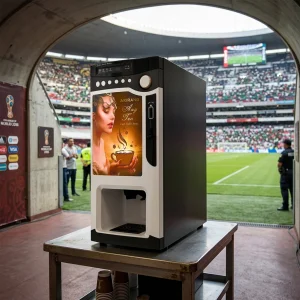
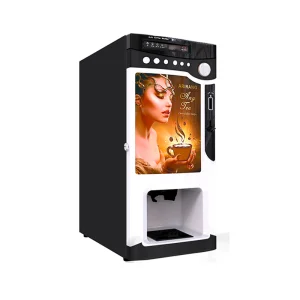
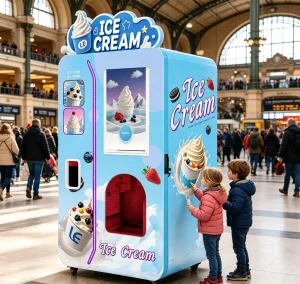
We offer light customization, on-demand engineering, sample processing, and graphic/touchscreen UI branding. Our 15 senior R&D engineers collaborate directly with global brand businesses and wholesalers to meet specific regional voltage, safety, and operational requirements.
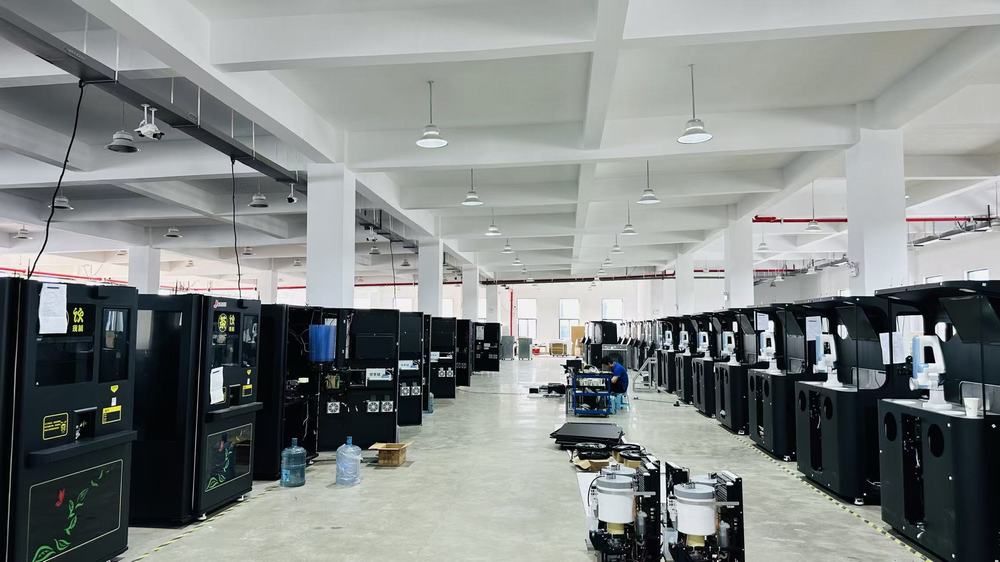
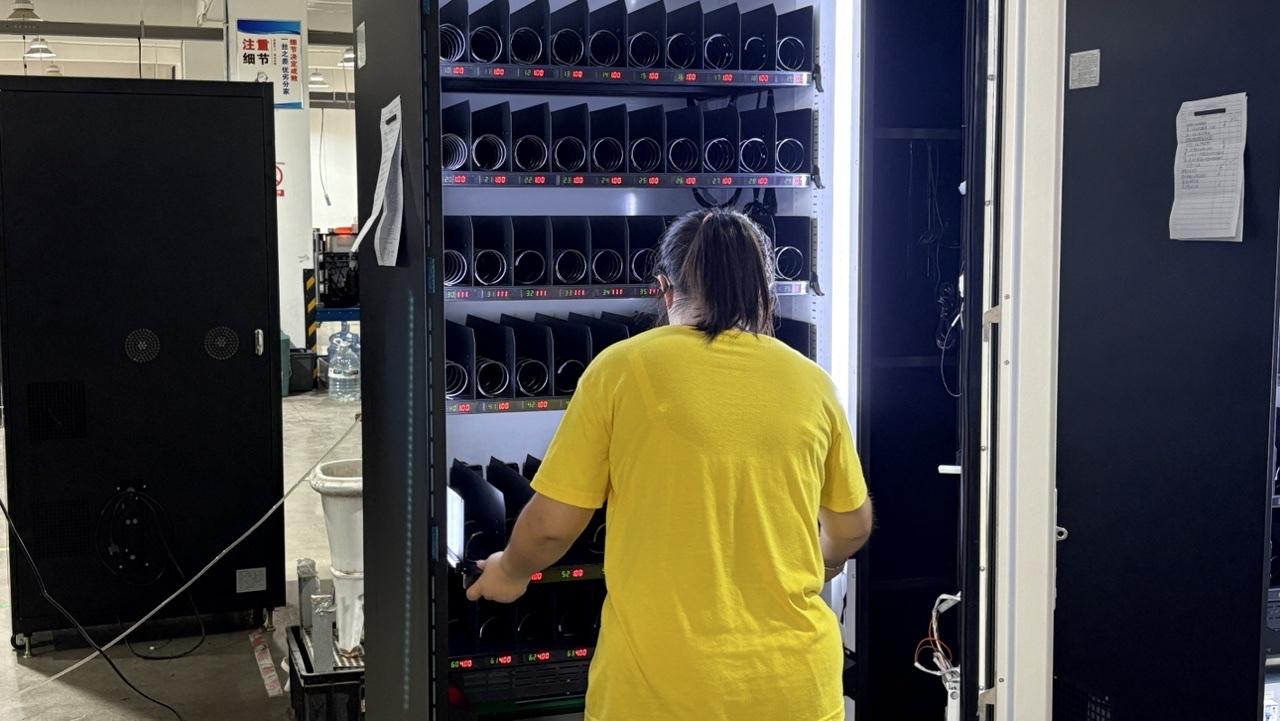
All our products adhere to international standards such as IEC 60335 electrical safety, ISO 9001 quality management, and ISO 14001 environmental standards. Every unit undergoes 100% full inspection across our 6 advanced production lines.
With 19 years of global export experience, our primary markets include Southeast Asia (35%), North America (10%), and various international regions. Our dedicated export team provides professional communication in English, Spanish, Italian, and Russian.
Operating across a 32,496 square meter facility with 6 high-efficiency manufacturing lines, we achieve a total annual output of 134,000 units, ensuring stable, timely, and scalable order fulfillment for global wholesalers and retailers.