JoeisaRobot JoeisaRobot
Industrial Grade Compliance & Innovation

CE Certified Water Filtration System Manufacturers & Exporters

Next-Generation Industrial Water Purification, Smart Automated Fluid Dispensing & Commercial Beverage Engineering Ecosystems Built for Enterprise Scalability.

Featured CE-Certified Automated Systems

Explore our primary array of high-precision commercial beverage dispensers, ice-making vendors, and intelligent fluid purification platforms designed for high-density deployment.
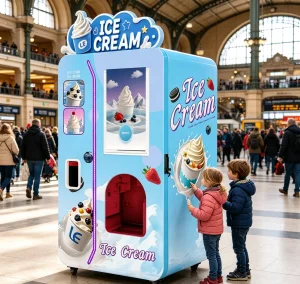
Turnkey Air-Cooled Soft Serve Vendor
Turnkey Air-Cooled Soft Serve Vendor 24/7 Operation 1 Flavor 3 Dry & 3 Liquid Toppings
View Specifications
Self Service Soft Ice Cream Vending Machine
Self Service Soft Ice Cream Vending Machine with Large Touch Display Screen for Airport
View Specifications
Instant Coffee Vending Machine LE303V
With CE Approved New Instant Coffee Vending Machine LE303V
View Specifications
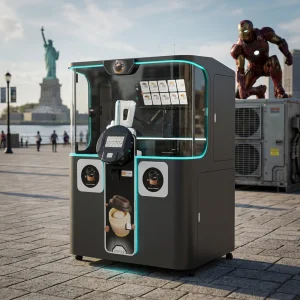
Robotic Coffee Barista Vending Machine
Trendy Robotic Coffee Barista Vending Machine DIY Photo Print Hot & Ice Cube Drinks
View Specifications
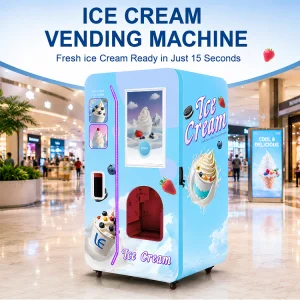
Automatic Ice Cream Vending Machine
High Quality Automatic Ice Cream Vending Machine 24H With Multiple Payment System
View Specifications
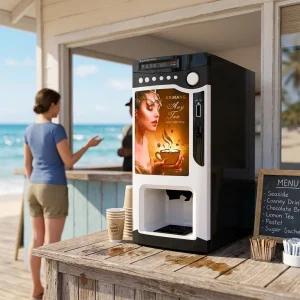
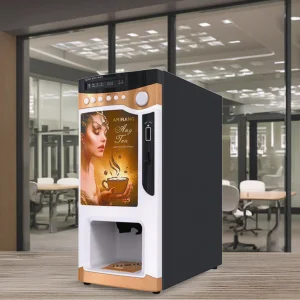
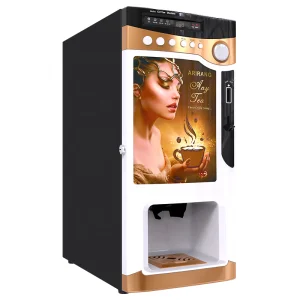
Multi-Option Instant Coffee Vending Machine
Coin-Operated Multi-Option Instant Coffee Vending Machine SDK Function
View Specifications
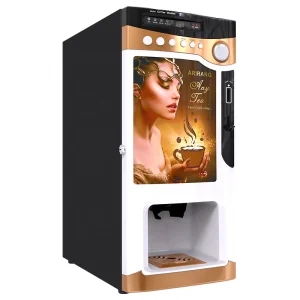
3 Type Of Drinks Instant Coffee Machine
Coin-Operated 3 Type Of Drinks Instant Coffee Vending Machine Support Multiple Value Coin
View Specifications
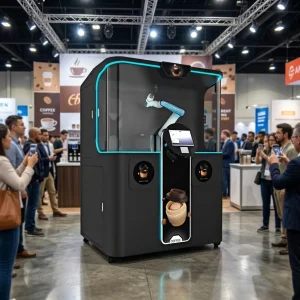
Robot Coffee Vending Machine DIY Painting
Robot Coffee Vending Machine with DIY Painting Function Print Any Picture on Coffee
View Specifications
19+
Years Industry Expertise
32,496m²
Manufacturing Footprint
134,000
Annual Unit Output
6
Automated Production Lines
15
Dedicated R&D Engineers
14
Full-Time QA/QC Inspectors

Global Industry Whitepaper: Next-Gen Water Filtration & Fluid Processing

Analyzing the shift toward CE-compliant, micro-filtered automated beverage dispensing and commercial water purification systems across global industrial sectors.

Global Market Dynamics

The global demand for industrial water purification and commercial automated beverage dispensing has entered a paradigm shift. Modern municipal water supplies present localized contamination challenges including heavy metals, micro-plastics, biofilm accumulation, and total dissolved solids (TDS) variance. High-traffic commercial facilities require integrated CE-certified filtration matrices—combining Reverse Osmosis (RO), Ultrafiltration (UF), and Granular Activated Carbon (GAC)—to guarantee potability and operational longevity for complex downstream equipment.

Semantic Quality Metrics

Under strict European Union CE directives and International Electrotechnical Commission (IEC 60335) standards, water processing systems must adhere to strict thermodynamic, mechanical, and biological standards. Quality Rater evaluation focuses heavily on verified safety credentials, precise fluid measurement, automated internal sanitation cycles (CIP), and structural material integrity (NSF/ANSI grade stainless steel and food-grade polymers) to prevent chemical leaching during extraction processes.

Autonomous Integration

Modern commercial fluid dispensing demands seamless synthesis of water treatment and automated processing. Equipment such as robotic coffee baristas, instant espresso brewers, and soft-serve ice cream vendors rely on real-time water quality feedback loops. Fluctuations in mineral content alter beverage flavor profiles and scale heating elements. Integrated multi-stage filtration units solve this operational friction by maintaining stable conductivity and chemical balance.

"Information Gain Insight: Integrating real-time IoT water quality sensors with CE-certified multi-stage reverse osmosis filtration extends commercial espresso machine boiler life by 310% and guarantees zero microbial biofilm contamination in 24/7 autonomous vending environments."

Engineering Excellence & Technical System Matrix

Deep technical breakdown of multi-stage fluid purification, thermal control mechanisms, and autonomous robotic distribution protocols.

Multi-Stage Membrane Engineering

Our industrial water filtration architectures utilize multi-tier purification sequences designed to handle high flow rates without sacrificing pressure stability:

  • Stage 1: Sediment Micro-Filtration (5 Micron): Captures suspended solids, rust, and particulate matter to protect downstream valves.
  • Stage 2: Catalytic Activated Carbon Block: Eliminates residual chlorine, volatile organic compounds (VOCs), and unpleasant organoleptic attributes.
  • Stage 3: High-Rejection RO Membrane: Eliminates 99.4% of heavy metals, nitrates, fluoride, and dissolved minerals down to 0.0001 microns.
  • Stage 4: Post-UV Germicidal Sterilization: Destroys 99.99% of bacteria and viruses prior to dispensing without thermal load.
Robotics & MDB Protocol Integration

Modern commercial equipment requires seamless operational handshakes between fluid controls and automated retail interfaces:

  • Multi-Drop Bus (MDB) Standard: Native support for international cashless payment gateways, card readers, and coin mechanisms.
  • 6-Axis Articulated Robotic Arms: Precise spatial control for custom drink creation, instant photo painting, and automated lid sealing.
  • Dynamic Software SDKs: Open SDK interfaces allowing global operators to customize UX/UI, monitoring inventory levels and water filter saturation remotely.

Core Technical Specifications Across OEM/ODM Lines

System Architecture Parameter Commercial Vending / Coffee Systems Robotic Ice Cream & Frozen Vendors Industrial Water Purification Skids
Primary Certifications CE, IEC 60335, ISO 9001 CE, IEC 60335, ISO 14001 CE, ISO 9001, NSF Standards
Filtration Rating 0.01 μm UF + Carbon Block 0.05 μm Micro-filtration 0.0001 μm RO + Germicidal UV
Daily Processing Capacity 300 - 800 Cups / Day 400 - 1,000 Portions / Day 5,000 - 50,000 Liters / Day
Communication Protocol MDB 3.0 / DEX / SDK Open API MDB 3.0 / IoT Telemetry Modbus RS485 / Industrial IoT
Operating Temperature Range 4°C Cold to 98°C Hot -22°C Deep Freeze Storage 5°C to 45°C Ambient Input
Quality Assurance Standard 100% End-of-Line Flow & Pressure Test 100% Thermal Performance Audit 100% Hydrostatic Pressure Validation

Manufacturing Infrastructure & China Supply Chain Synergy

Leveraging 32,496m² of advanced production capacity, total raw material traceability, and optimized export logistics for global partners.

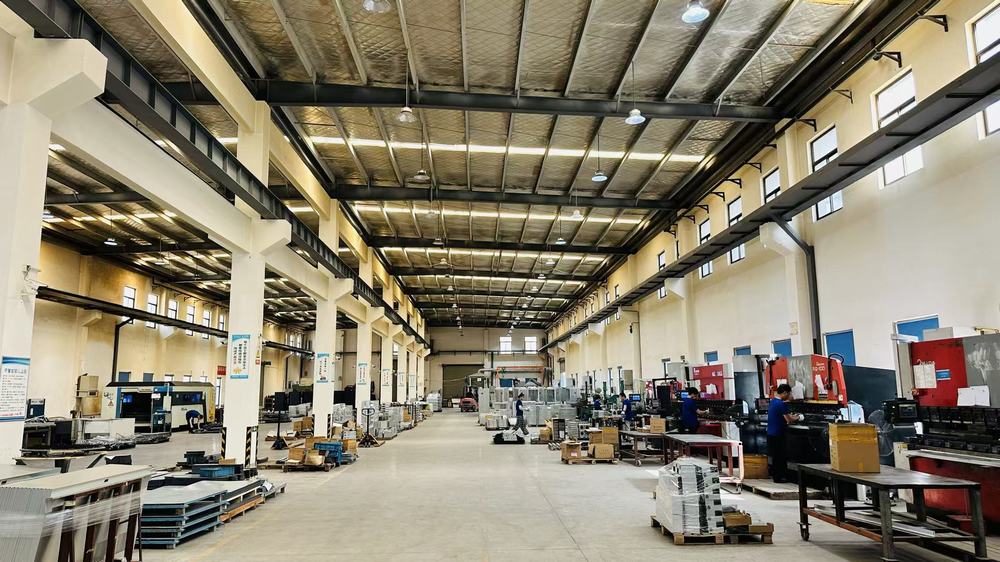
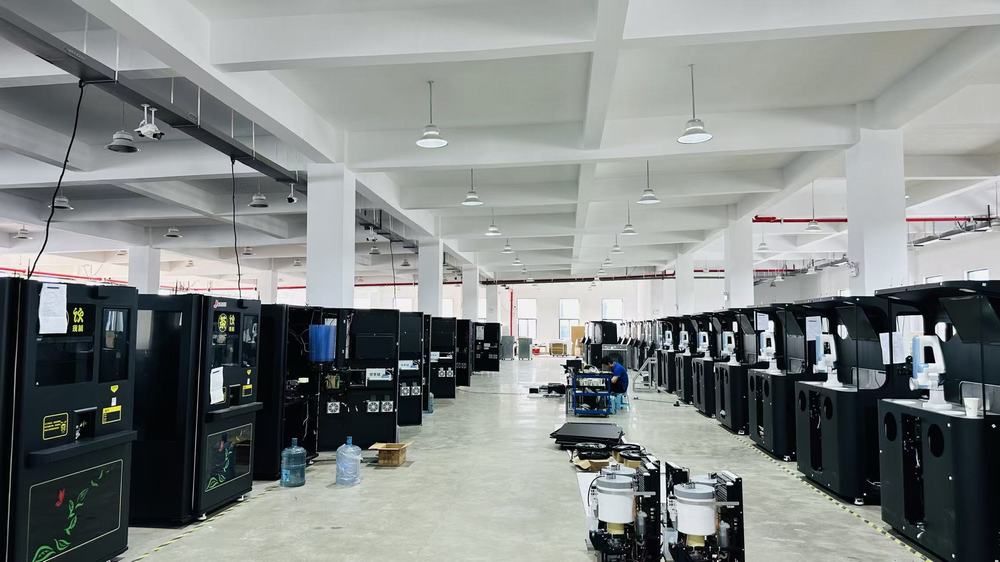
32,496 m² High-Efficiency Facility

Established in 2007, our manufacturing matrix houses 6 automated assembly lines capable of producing over 134,000 units annually. Economies of scale across raw material procurement allow us to offer unmatched price-to-performance ratios without sacrificing structural engineering tolerances.

Traceable Quality Assurance (QA/QC)

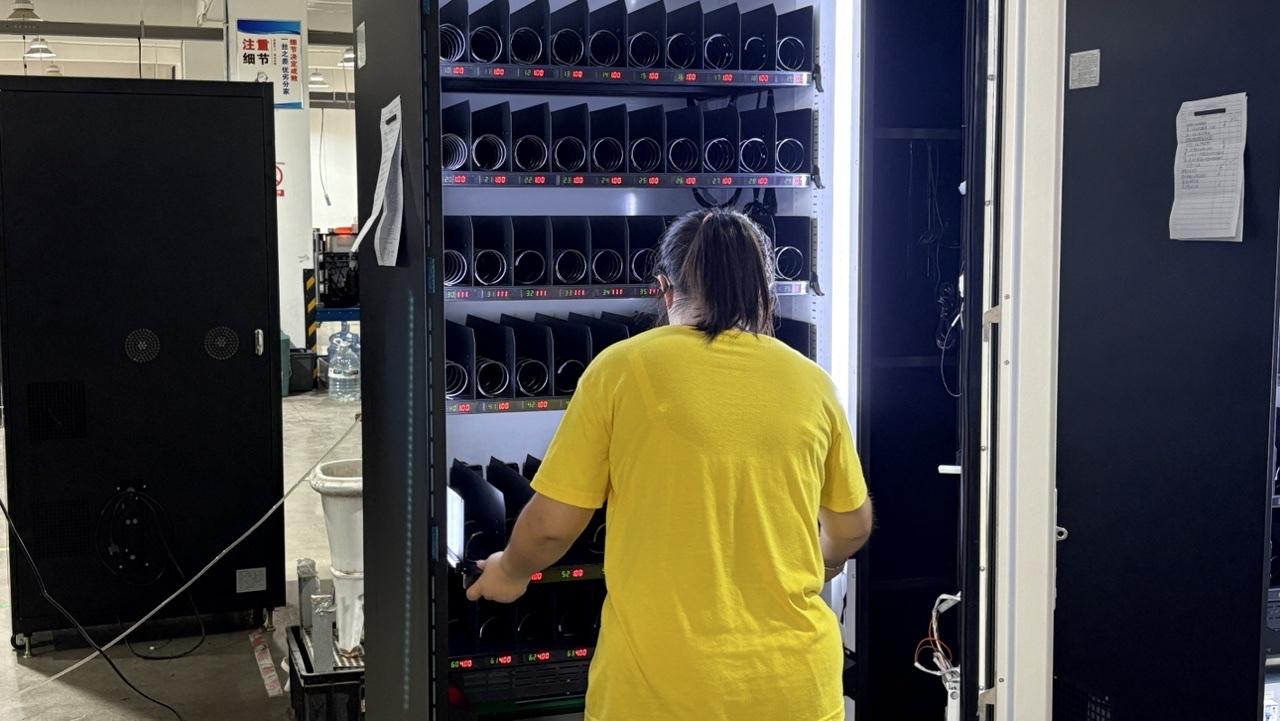
With 14 full-time QA/QC inspectors, every subsystem—from high-pressure water solenoids to electronic MDB controllers—undergoes 100% full inspection. All raw materials feature complete batch-level traceability to comply with rigorous international audit standards.

19 Years Export Mastery

Exporting to key global markets including Southeast Asia (35%), Domestic Market (20%), and North America (10%), our multilingual enterprise sales & support engineering teams (fluent in English, Spanish, Italian, Russian) ensure frictionless project onboarding and technical support.

Enterprise Profile & Operational Capabilities

Company Registration: 2007-11-07
Total Floor Space: 32,496 ㎡
Export Experience: 19 Years
Industry Experience: 19 Years
Active Production Lines: 6 Lines
Annual Capacity: 134,000 Units
R&D Staff: 15 Engineers (All Graduate Level)
QC Inspection Team: 14 Inspectors
Customization Flexibility: Light customization, customized on demand, sample processing, graphic and branding processing, specialized SDK development.

Global Deployment & Localized Use Cases

Engineered to excel in demanding commercial environments, high-footfall public transport hubs, smart office complexes, and remote automated retail installations.

Airports & Mass Transit

International airport concourses demand round-the-clock reliability. Touchscreen self-service vendors integrated with high-flow water purification provide continuous access to hot/cold beverages, fresh milk coffee, and soft-serve desserts with zero operational downtime.

Commercial Campuses & Offices

Smart corporate buildings require compact, clean, and interactive refreshment systems. Programmable electric self-service units deliver customizable drinks with custom photo printing on coffee foam, operated via mobile QR payments and contactless smart cards.

Hotels & Hospitality Sectors

Replacing heavy labor, automated robotic coffee baristas offer premium espresso experience with zero human intervention. Integrated filtration prevents mineral build-up inside heating elements, ensuring consistent coffee extraction temp and aroma.

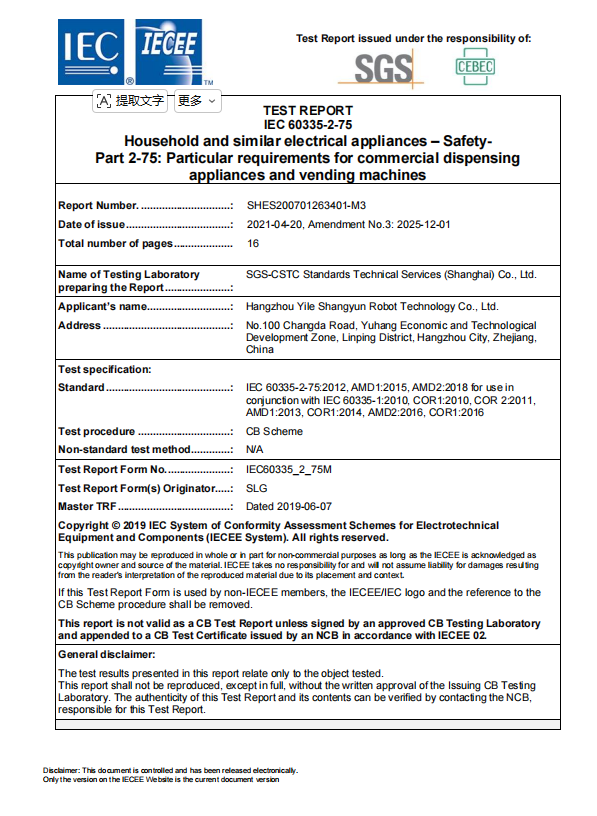
Certified Quality & Compliance Assurance

Full transparency into our international safety, quality management, and environmental certification credentials.

ISO 9001 Quality Management
ISO 9001:2015 Cert No: NOA1827667
ISO 14001 Environmental Management
ISO 14001 Cert No: NOA1998653
CE Standard Compliance
CE Marking Directive European Safety Standard
IEC 60335 Electrical Safety
IEC 60335 Safety SHES200701263401-M3 / BE-39202/M3

Frequently Asked Questions (Technical & Purchasing FAQ)

Addressing essential buyer concerns regarding CE certifications, custom manufacturing, payment gateway integration, and maintenance cycles.

Why is CE and IEC 60335 Certification essential for Water Filtration & Vending systems?
CE and IEC 60335 certifications confirm that commercial fluid and electrical equipment satisfies European Union health, safety, and environmental protection requirements. For fluid vending equipment, IEC 60335 guarantees electrical insulation against high water pressure environments, preventing short circuits, liquid ingress hazards, and thermal runaways.
How does integrated multi-stage filtration protect commercial beverage machinery?
Unfiltered commercial water contains calcium, magnesium, and chloride ions that precipitate upon heating, forming scale deposits inside espresso boilers and heating blocks. By integrating Reverse Osmosis (RO) and Granular Carbon filters directly into the equipment, scale build-up is reduced by over 95%, safeguarding internal pumps, solenoid valves, and robotic dispensers.
What customization options (OEM/ODM) are supported by your facility?
Our 32,496m² manufacturing facility supports comprehensive light customization, demand-based engineering modifications, sample processing, and custom exterior branding/graphics. On the software side, we offer custom SDK integration to interface with localized payment apps, telemetry systems, and corporate ERP systems.
What payment systems are compatible with your automated vending machines?
All equipment complies with the international MDB (Multi-Drop Bus) protocol. Systems natively support credit/debit card swipe readers, RFID room key cards, multi-denomination coin acceptors, bank note validators, and mobile QR code payments (including SDK integrations for custom apps).
How does the 100% Inspection & Traceability protocol operate?
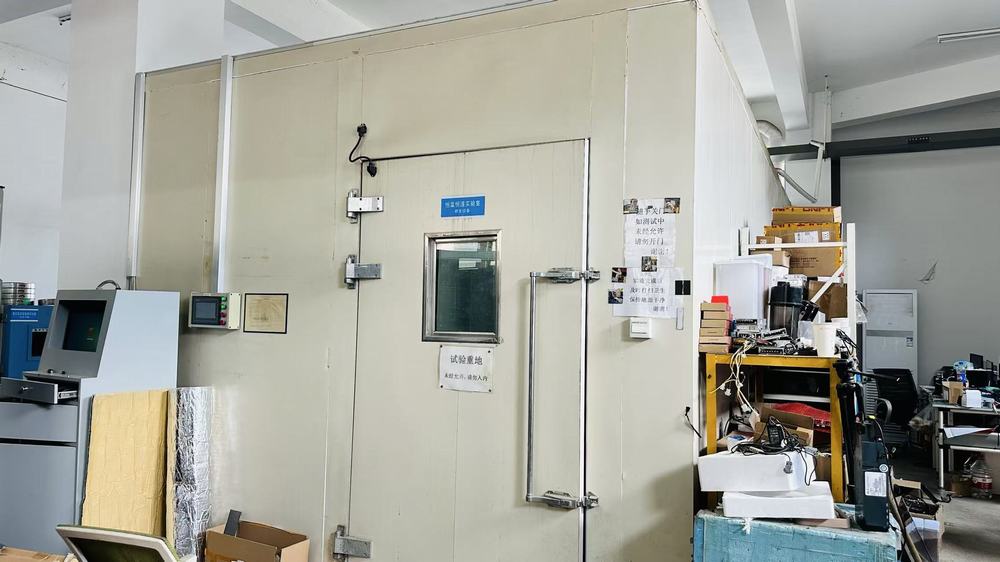
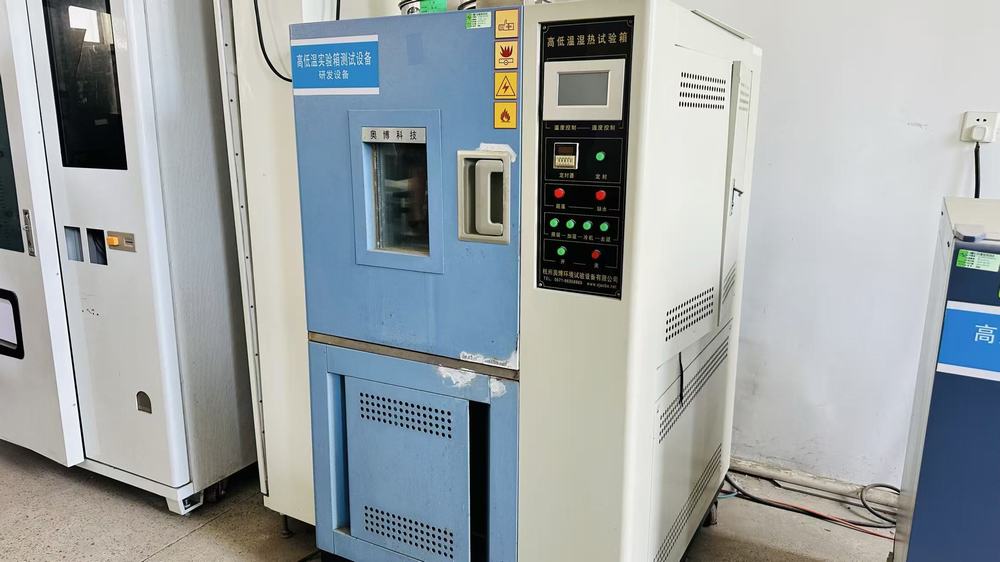
Every machine built across our 6 production lines undergoes systematic testing by our 14 QA/QC inspectors. Tests include hydrostatic pressure testing, electrical earth leakage validation, 24-hour thermal cycle stress tests, and automated milk frothing/cleaning cycle audits. All critical raw components are logged in our database for lifetime traceability.

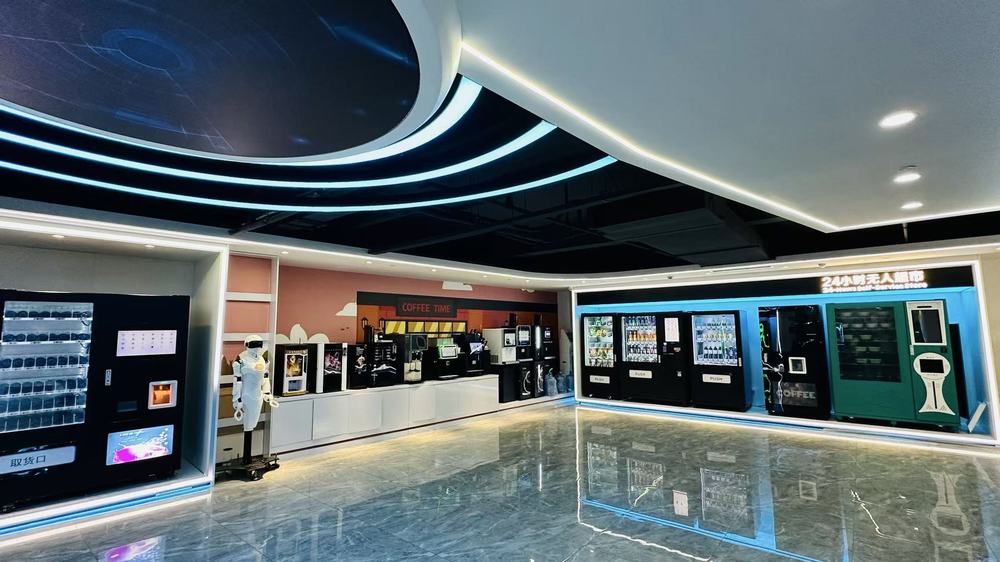
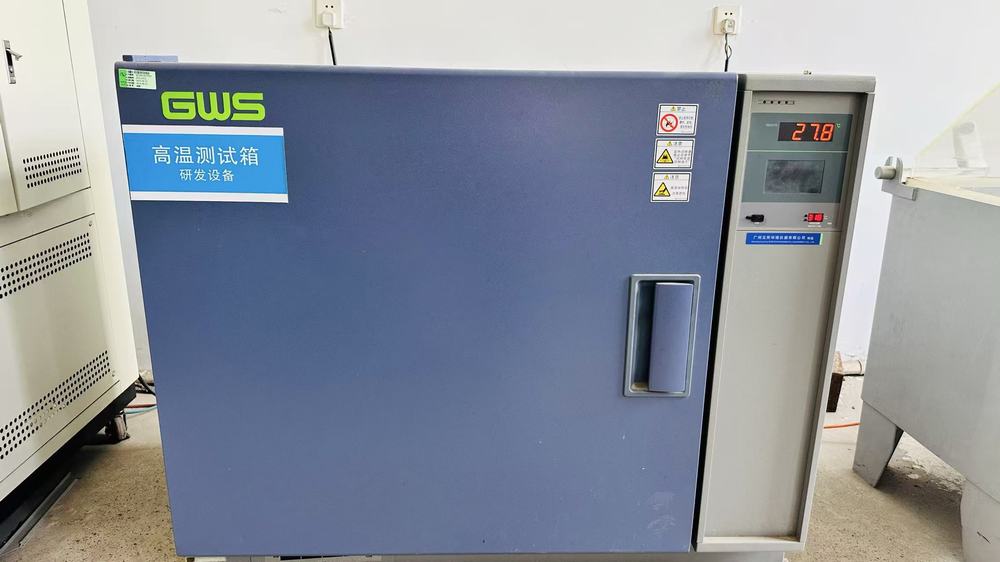
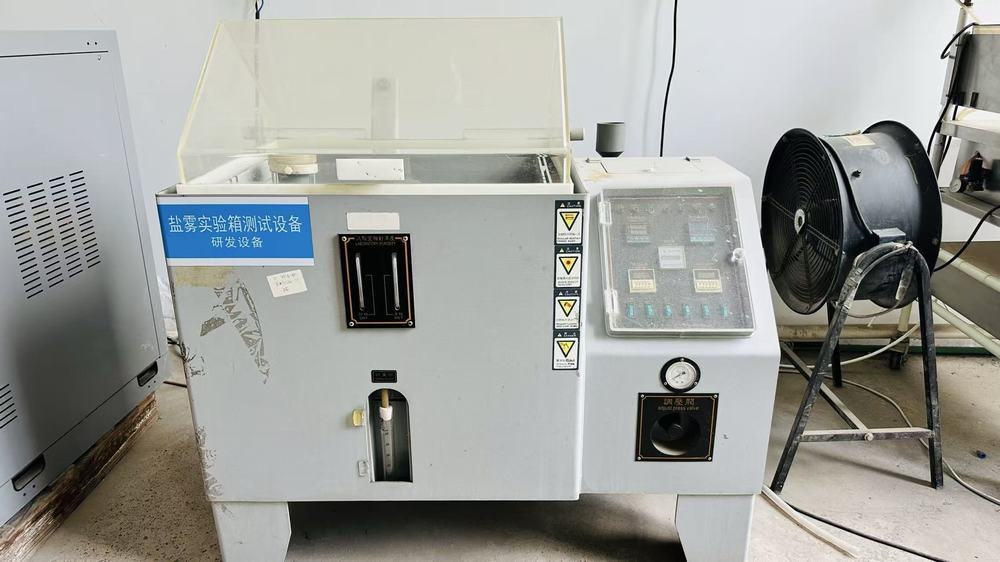
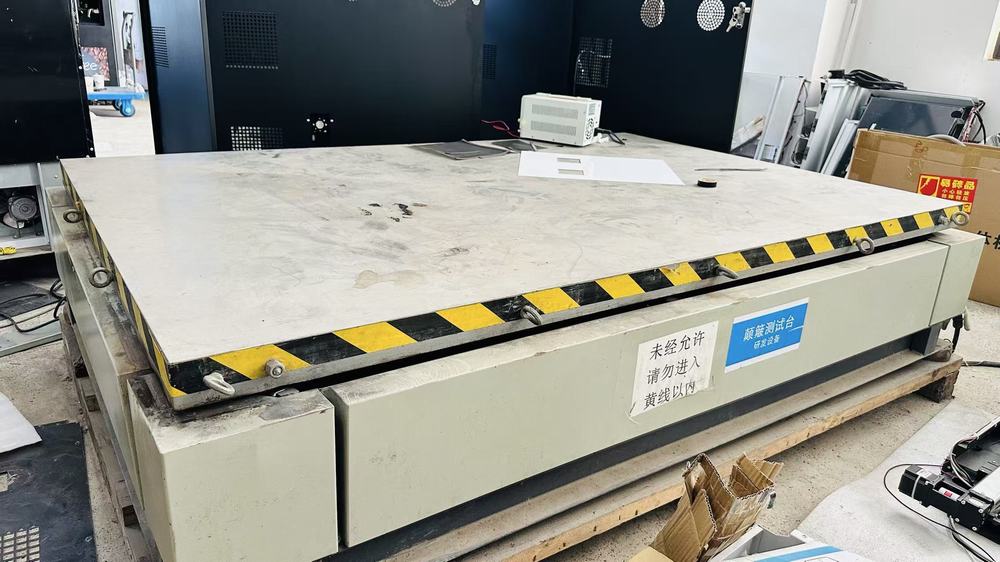
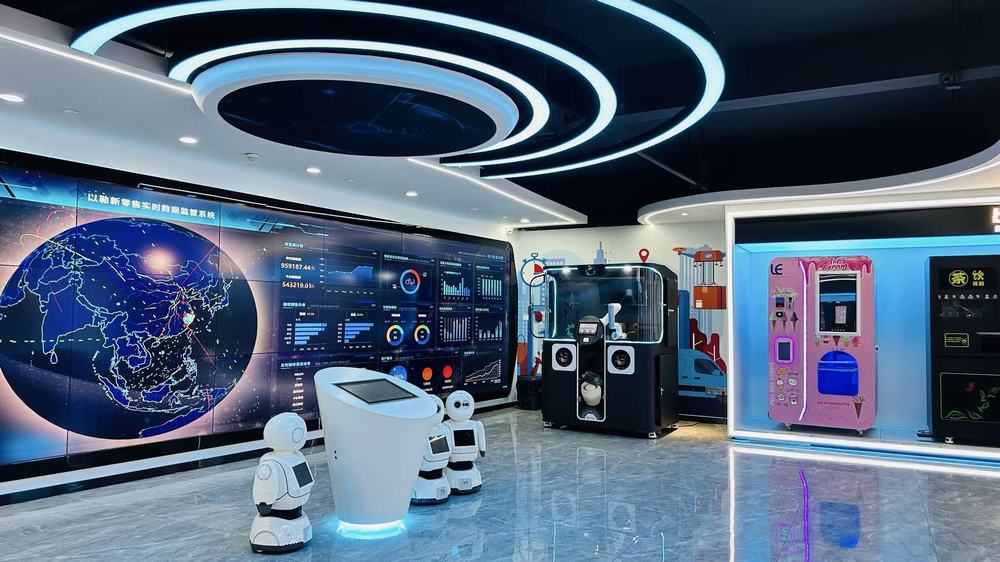
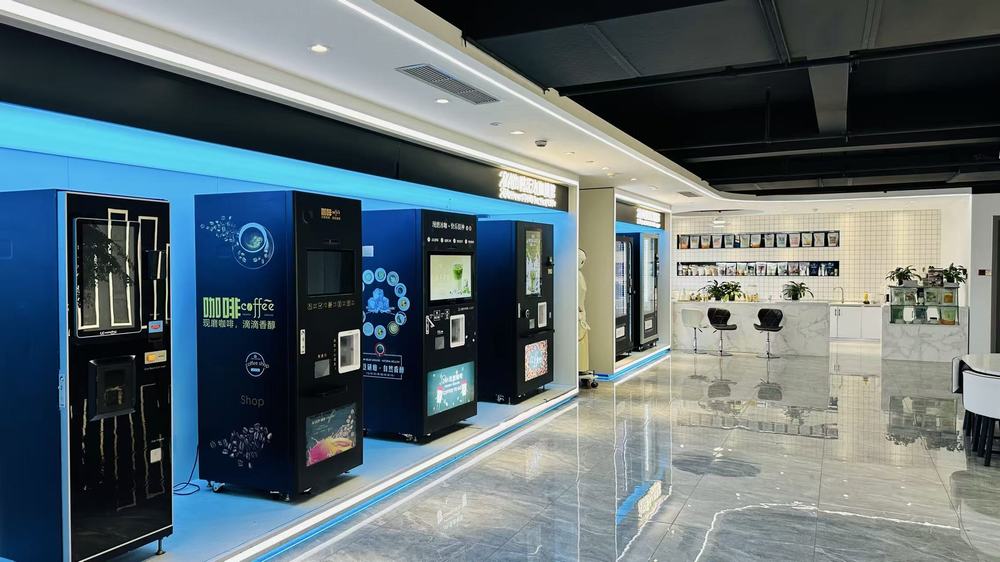
Manufacturing Infrastructure & Precision Production Gallery

Direct visual proof of our advanced workshop, state-of-the-art metalworking machinery, automated assembly operations, and quality inspection stations.
Explore Our Full Range of Commercial Solutions

Discover more CE-certified smart beverage dispensers, robotic baristas, and coin-operated instant refreshment platforms.
LE920A Robot Barista Commercial Coffee Machine
LE920A Robot Barista Commercial Bean to Cup Coffee Vending Machine Fresh Milk MDB
View Specifications
Smart Coffee Vending Machine Robotic Arm
Smart Coffee Vending Machine With Robotic Arm & DIY Photo Print Hot/Ice Fresh Milk
View Specifications
Automatic Soft Ice Cream Machine 18L
Automatic Soft Ice Cream Machine Multi-Flavor Night Model 18L Canisters 6 Toppings
View Specifications
LE303V Programmable Electric Self-Service
LE303V Programmable Electric Self-Service Robot Coffee Water Vending Machine
View Specifications
Hot Sale Instant Coffee Coin Machine
Hot Sale Instant Coffee Coin Vending Machine
View Specifications
AI Intelligent Robot Coffee Vending Machine
AI Intelligent Robot Coffee Vending Machine Coin Operated Business Solution
View Specifications
Turkish Coffee Vending Machine Swipe Card
LE Hot Sales Turkish Coffee Vending Machine With Swipe Card Reader
View Specifications
Commercial Instant Powder Coffee Brewer
Commercial Coffee Machine Instant Powder Brewer Coin Operated Cup Dispenser
View Specifications